Description
Salient Features
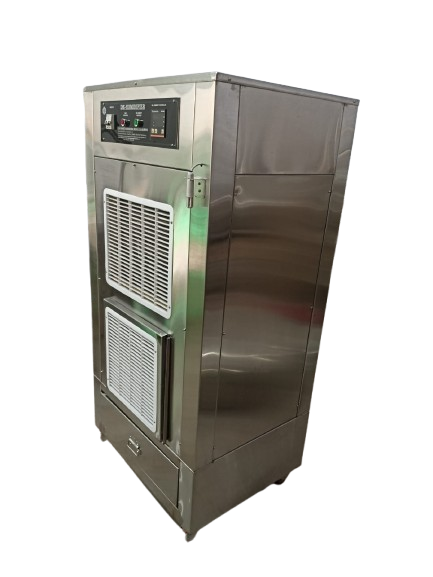
- cGMP & WHO-GMP compliant construction
- Available in 1 TR, 1.5 TR & 2 TR capacities
- High moisture removal efficiency
- Digital Temperature & Relative Humidity (RH) Controller
- Heavy-duty hermetically sealed Rotary/Scroll compressor
- Eco-friendly refrigerant
- High-efficiency copper evaporator and condenser coils
- Industrial centrifugal blower for uniform airflow
- Powder-coated MS or SS 304 cabinet construction
- Washable synthetic pre-filter
- Automatic condensate drainage system
- Low noise and vibration operation
- Energy-efficient refrigeration system
- Suitable for 24×7 continuous industrial operation
- Easy installation, servicing, and maintenance
- Floor-mounted compact design
- Designed for pharmaceutical cleanroom applications
Working Principle
The TECHMAC GMP Dehumidifier operates on the refrigeration dehumidification principle. Moist air is drawn into the unit through a high-capacity centrifugal blower and passes over a low-temperature evaporator coil. As the air temperature drops below its dew point, water vapour condenses into liquid form and is automatically drained through the condensate drainage system.
The dehumidified air is then reheated naturally through the refrigeration cycle and discharged back into the room, maintaining the desired humidity level while ensuring a comfortable process temperature. This process effectively protects moisture-sensitive products and ensures stable production conditions.
Technical Specifications
| Model | TEW-1TR | TEW-1.5TR | TEW-2TR |
| Cooling Capacity | 1 TR | 1.5 TR | 2 TR |
| Moisture Removal Capacity* | 25–30 L/Day | 40–50 L/Day | 60–70 L/Day |
| Air Flow | 600–800 CMH | 1200–1500 CMH | 1800–2500 CMH |
| Humidity Control Range | 20%–60% RH | 20%–60% RH | 20%–60% RH |
| Operating Temperature | 18°C–35°C | 18°C–35°C | 18°C–35°C |
| Refrigerant | Eco-Friendly Refrigerant | Eco-Friendly Refrigerant | Eco-Friendly Refrigerant |
| Compressor | Hermetically Sealed Rotary / Scroll | Hermetically Sealed Rotary / Scroll | Hermetically Sealed Rotary / Scroll |
| Power Supply | 230V AC / Single Phase | 415V AC / Three Phase | 415V AC / Three Phase |
| Frequency | 50 Hz | 50 Hz | 50 Hz |
| Cabinet Material | Powder Coated MS / SS 304 | Powder Coated MS / SS 304 | Powder Coated MS / SS 304 |
| Control System | Digital Temperature & RH Controller | Digital Temperature & RH Controller | Digital Temperature & RH Controller |
| Mounting | Floor Mounted | Floor Mounted | Floor Mounted |
* Moisture removal capacity varies depending on ambient temperature and humidity conditions.
Standard Construction
| Component | Material / Description |
| Main Cabinet | Powder Coated Mild Steel / SS 304 |
| Evaporator Coil | Copper Tubes with Aluminium Fins |
| Condenser Coil | Air-Cooled Copper Condenser |
| Compressor | Hermetically Sealed Rotary / Scroll |
| Blower | Heavy Duty Centrifugal Blower |
| Air Filter | Washable Synthetic Pre Filter |
| Controller | Digital Temperature & Humidity Controller |
| Drain System | Automatic Condensate Drain |
| Base Frame | Heavy Duty Welded Construction |
| Electrical Panel | Industrial Grade Components with Safety Protection |
Applications
Pharmaceutical Industry
- Capsule Filling Rooms
- Tablet Compression Rooms
- Granulation Areas
- Coating Rooms
- Packaging Departments
- API Manufacturing Areas
- Raw Material Stores
- Stability Chambers
Nutraceutical Industry
- Capsule Manufacturing
- Powder Blending
- Tablet Production
- Packaging Rooms
Food Industry
- Spice Processing Plants
- Milk Powder Production
- Dry Food Packaging
- Bakery Ingredient Storage
- Tea & Coffee Processing
Cosmetic Industry
- Face Powder Manufacturing
- Cosmetic Filling Areas
- Packaging Sections
- Raw Material Warehouses
Chemical Industry
- Hygroscopic Chemical Processing
- Fine Chemical Manufacturing
- Controlled Humidity Storage
- Laboratory Applications
Optional Accessories
- PLC Based Automation
- 7″ Touch Screen HMI
- HEPA Filtration System
- Complete SS 304 Construction
- SS 316 Internal Components (where applicable)
- Auto Restart Function
- Building Management System (BMS) Integration
- Data Logger
- Differential Pressure Gauge
- Remote Monitoring System
- Temperature & Humidity Recorder
- DQ, IQ, OQ & PQ Validation Documentation
Advantages
- Accurate humidity control for critical manufacturing environments
- Prevents moisture absorption and product degradation
- Improves product quality and shelf life
- Reduces microbial growth caused by excess humidity
- Energy-efficient and low operating cost
- Rugged industrial construction for long service life
- Easy maintenance with readily accessible components
- Reliable 24×7 continuous operation